Precautions.
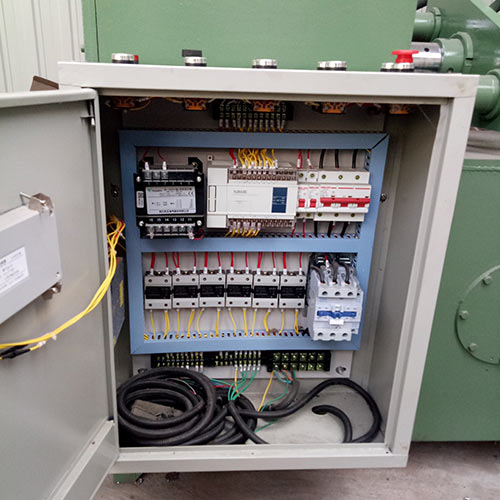
- Condensation can form on the contactors when humidity changes — take measures to prevent phase-to-phase short circuits.
- Keep the machine clean, especially between incoming and outgoing phases.
- Inspect, service and maintain the machine regularly.
- Carry out a full overhaul every 5,000 operating hours.
- Check all fasteners for looseness regularly.
- Stop the machine on any abnormal noise, clear the fault, then restart.
- Replace the die when wear causes bent or out-of-tolerance reduced ends.
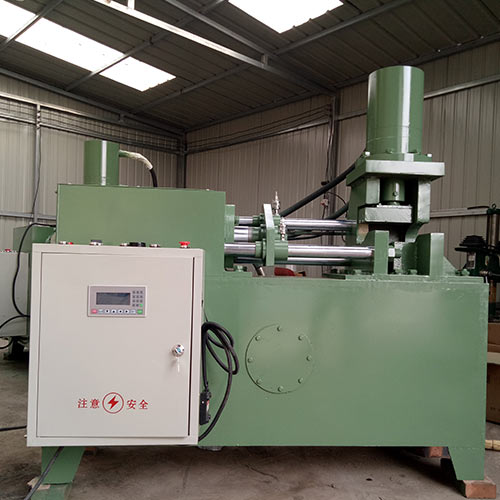
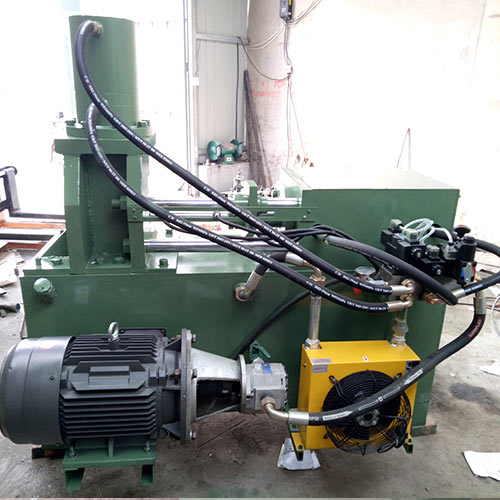
Applications and features. A chipless machine: hydraulic force drives the part into a dedicated die and it is cold-reduced in a single stroke. It is productive, simple to operate, economical in material and consistent in quality. The reduced section becomes denser, raising compressive strength while keeping plasticity and impact toughness. It compresses 3–5 parts per minute — 3–5 times faster than turning — and 2,000–3,000 pieces per shift, which suits volume production. Diameter, roundness and taper errors stay within 0.03 mm, surface finish is good, and parts extend 10–15%, saving steel: a 20 mm bar at 864,000 pieces a year saves about 30 tonnes.
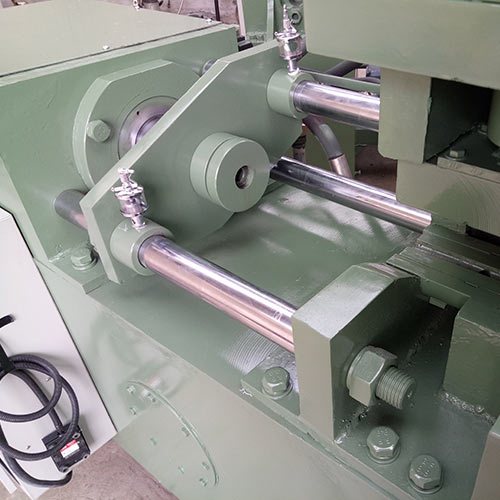
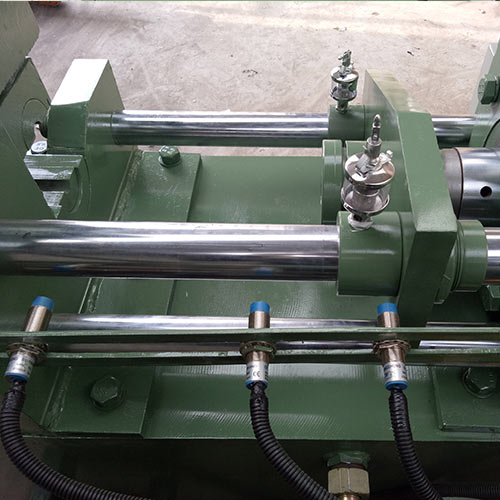
Installation and adjustment. Use the lifting points with a padded wire rope. Stand the machine on a level, solid floor; pour concrete where there is shock or vibration. After connecting power, check motor rotation and set the limit switch for the reduced length required. Set hydraulic pressure as low as the job allows — finer diameters need less pressure. To change the die, loosen the front screws, remove the cover and tap the die out from the rear with a soft wedge (never strike the carbide), then refit and tighten. To change clamping blocks, open the cylinder cover, withdraw the pins, swap blocks by number and reassemble; clean and oil the old blocks as spares.
Troubleshooting. Gauge needle vibrating — clean the blocked oil intake. Vibration on feed or return — bleed air from the cylinder or top up slide lubrication. Oil overheating — reduce viscosity, shorten feed time, lower pressure or add a cooler. Pressure will not build — replace a worn pump, change thin oil, replace a faulty relief valve or worn coupling. Contactor humming — clean the core faces. Breaker tripping — check for short circuit, burnt motor, broken supply line or a stuck button. Loss of power on inching — check the contactor holding circuit, contacts, plugs and stop button. Failure to stop — replace welded contacts or a damaged button, clean oily core faces.
 Public Security Filing No. 13052502000329

 Official WeChat


